Product Code: 8934A

Superdie I / Zamak 2 Zinc Base Alloy

4-20 lb Ingot Format Easy Castability High Ductility Rubber Mold Compatible
Zinc-base rubber mold casting alloy in 4-20 lb ingot form. Easy to cast and highly ductile. Used for die casting and sculpture applications.
Primary Elements
Zn
Custom request

Can't find the right composition?

Product Overview

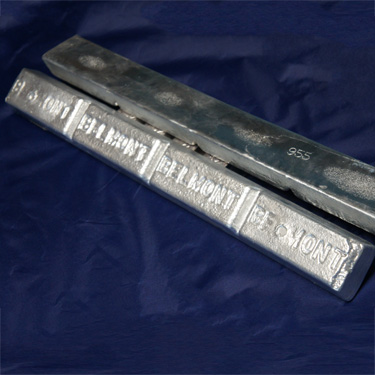
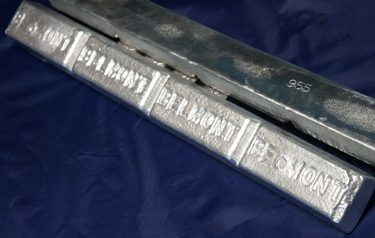
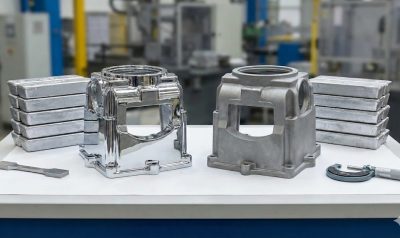
Zinc Base Alloy (8934A) in 4-20 lb ingot form is a highly ductile zinc-based casting alloy supplied in the standard 4-20 lb ingot format compatible with zinc casting melting pots used in die casting and sculpture production. The ingot weight range accommodates both small bench-top pots for craft and low-volume work and larger production melting furnaces. The easy castability of this alloy makes it tolerant of temperature variation in less-controlled melting setups, and its high ductility allows post-casting forming and assembly operations without risk of cracking. The 4-20 lb ingot format is the standard charge unit for rubber mold casting operations, providing a manageable addition size that minimizes pot temperature disruption when replenishing the melt during production. Supplied as 4-20 lb ingots.

Available Forms

4-20 Ingot

Product Code

8934A

Technical Info

Physical Properties

Primary ElementsZn
Performance tags
4-20 lb Ingot FormatEasy CastabilityHigh DuctilityRubber Mold Compatible

Frequently Asked Questions

Common technical inquiries regarding Superdie I / Zamak 2 Zinc Base Alloy
Zinc-base rubber mold casting alloys are typically poured at 700-850F for gravity casting, with the specific temperature depending on mold complexity and section thickness. Thinner sections and more complex mold geometries require higher temperatures for complete fill, while simple thick-section pours can use lower temperatures that extend mold life.
Zinc ingots should be stored dry to prevent white rust (zinc carbonate/zinc oxide surface oxidation from moisture exposure), which is cosmetic but can introduce oxide inclusions if corroded surfaces are melted without cleaning. Covered indoor storage on pallets above floor level is adequate for most conditions.
The melting equipment is compatible, but the alloys should not be mixed as they have different compositions and properties. Before switching from S1/J1 to this alloy, the melting pot should be fully drained and cleaned to remove residual Kor-Zee alloy. Similarly, if switching back to Kor-Zee after using this alloy, a clean-out melt using scrap of the target alloy should be performed before introducing production-grade KZ ingots.

Safety Data (SDS)

Request a Quote

Complete our Quote form, and we'll respond with options for you!