1 lb Regular BarAutomotive and Radiator RepairGeneral Purpose Copper and Steel JoiningGeneral Purpose Joining
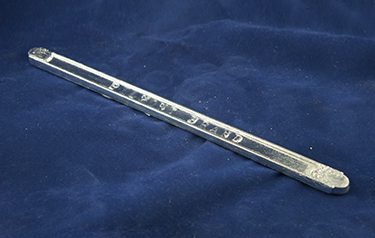
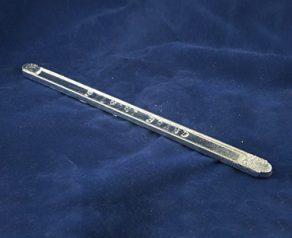
50% Sn / 50% Pb general purpose solder in regular bar and capping bar forms. Wide melting range. Used for automotive radiator, gutter repair, and electrical applications.
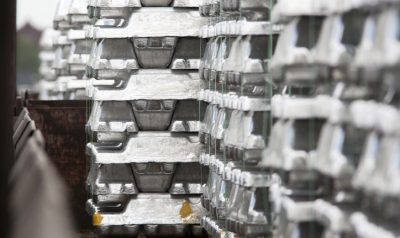
50/50 Tin-Lead General Purpose Solder is a classic solder alloy with equal parts tin and lead, providing a wide melting range suitable for general-purpose joining of copper, copper alloys, lead, nickel alloys, and steel. Tin-lead solders are the largest and most widely used group of soldering alloys, compatible with all types of base metal cleaners, fluxes, and heating methods. The 50/50 composition has a wider melting range than the near-eutectic 60/40 composition, which makes it useful for applications where the extended plastic (pasty) range between solidus and liquidus is advantageous, for example in automotive radiator repair and gutter work where the joint must be wiped or formed while the solder is partially solid. It is also used for electrical connections, plumbing, and general metal joining in industrial and repair applications. Available as regular bar and capping bar.
Available Forms
Capping Bar, Regular Bar
Product Code
75012
Technical Info
Thermal Properties
Melting Point (Solidus)361
Melting Point (Liquidus)421
Physical Properties
Density (imperial)0.321
Density (metric)8.89
Physical Properties
Primary ElementsPb, Sb, Sn
Lead FreeNo — contains lead
Performance tags
1 lb Regular BarAutomotive and Radiator RepairGeneral Purpose Copper and Steel JoiningGeneral Purpose JoiningWide Melting RangeWipeable Pasty Range
Nominal Composition
50% Sn
49.65% Pb
Bal
Frequently Asked Questions
Common technical inquiries regarding 50/50 Tin Lead Solder Alloy
The 60F spread between solidus (361F) and liquidus (421F) in 50/50 solder creates an extended pasty range where the alloy is partially solid and can be worked, wiped, and shaped with a paddle or cloth while still warm. This is essential for automotive body solder work and leaded gutter repair where joints must be built up and contoured to a smooth profile before the solder fully solidifies. The 60/40 near-eutectic composition freezes too quickly to be wiped effectively, making 50/50 the standard for these applications.
On copper and copper alloys, a rosin-based or mildly activated flux is sufficient to remove the thin copper oxide layer and promote solder wetting. On steel, a more aggressive flux such as a zinc chloride-based active flux or acid flux is required to penetrate the iron oxide layer and achieve wetting. After soldering steel with active flux, thorough flux residue removal with water is essential to prevent corrosion at the joint.
A capping bar is a short, flat solder bar cast to fit over the opening of a solder pot or crucible as a cover, serving as both a convenient storage form and a pre-measured charge unit. Capping bars are used in plumbing, stained glass work, and other trades where a solder pot is used intermittently and the bar is melted in place by heating the pot. The flat geometry also makes capping bars convenient for feeding into a soldering iron tip trough or ladle for manual joint work.
This Solder has good corrosion resistance and tensile strength. With a melting range beginning at 390 Deg. F. it avoids causing damage to critical electronics as well preventing substrate deformation and segregation. It is used very often in spray wire form for capacitors and other electronic parts.
60% Sn / 40% Pb near-eutectic solder in bar form. Used for delicate electronics, precision soldering, and applications where narrow melting range is critical.