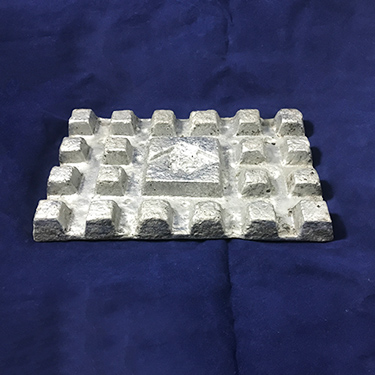
5% Phosphor Tin Alloy is a tin-phosphorus master alloy with a nominal composition of 95% Sn and 5% P. Phosphorus additions to tin and tin-based solder melts suppress dross formation by acting as an antioxidant — the phosphorus preferentially oxidizes at the melt surface, forming a thin protective oxide that inhibits the rapid bulk oxidation of the tin bath that produces heavy dross accumulation. This keeps the solder bath cleaner, reduces metal losses from dross skimming, and extends bath life in wave soldering and pot soldering operations. Phosphor tin is used in the electronics soldering industry, plumbing solder manufacturing, and bearing alloy production to maintain bath cleanliness and reduce operating costs. Forms: waffle form for convenient breaking and addition to solder and tin baths.
Available Forms
Waffle
Product Code
7955
Technical Info
Thermal Properties
Melting Point (Solidus)1,317°F (714°C)
Melting Point (Liquidus)1,542°F (839°C)
Physical Properties
Density (imperial)0.28 lbs/in³
Density (metric)7.75 g/cm³
Primary ElementsSn · P
Lead FreeYes
Key Features
Dross SuppressorTin Bath AntioxidantSolder Bath TreatmentReduces Metal Loss
Solubility Note
Dissolves readily in molten tin and tin-base solder baths at standard soldering temperatures; add in small increments to avoid excessive phosphorus buildup which can affect solder joint quality.
Nominal Composition
95% Sn
5% P
Frequently Asked Questions
Common technical inquiries regarding 5% Phosphor Tin Alloy
Addition rates for wave soldering bath maintenance are typically 0.005-0.02% P by weight of the solder bath, which requires 0.1-0.4% of the bath weight as 5% Phosphor Tin Alloy. Additions are made periodically as the phosphorus is consumed by oxidation during bath operation — the rate of consumption depends on bath temperature, exposure area, and throughput. Monitor bath chemistry regularly by spectrographic analysis and replenish phosphorus when the level drops below the target. Excessive phosphorus above approximately 0.05% P can affect solder joint wetting and intermetallic formation in electronic assemblies.
Phosphor tin additions must be used within the limits specified by the applicable solder alloy standard. IPC J-STD-006 specifications for tin-silver-copper and other lead-free solders set maximum phosphorus limits, typically below 0.01%. Additions above these limits can produce solder that fails specification even if the base alloy chemistry is correct. For wave soldering and selective soldering applications governed by IPC specifications, maintain phosphorus within the specification limit and document additions for process traceability. Confirm with your solder alloy specification before use.
Phosphor tin is used in both leaded and lead-free solder bath maintenance. Lead-free solder baths — particularly tin-copper grades used in wave soldering — are more prone to dross formation than tin-lead because the higher operating temperatures (typically 50-75°F above equivalent tin-lead baths) increase oxidation rates. Phosphor tin additions are therefore more important in lead-free wave soldering operations than in tin-lead. However the tighter chemistry specifications of lead-free solders require closer monitoring of phosphorus levels to remain within the applicable IPC specification limits.
Phosphor copper deoxidizer (85% Cu, 15% P) — the most widely used copper alloy deoxidizer. Effectively removes oxygen with minimal dross. Shot and waffle forms.
2% boron copper master alloy for deoxidizing pure copper or grain refining brass alloys. Forms: polished shot; unpolished shot; waffle; and 4-5 oz pieces.